Featured Wellhead & Severe-Duty Drive Motor Fleet
Precision-engineered artificial lift drives, heavy-duty three-phase vibration motors, and multi-layer screening power units tested under extreme load protocols.
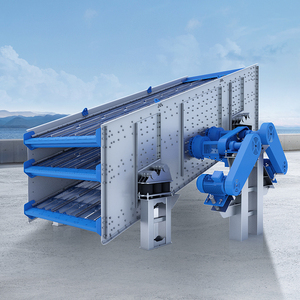
Aggregate Vibrating Screen Machine for Stone Crusher Plant 60-350t/h Ore Processing 30kW Motor
Send an Inquiry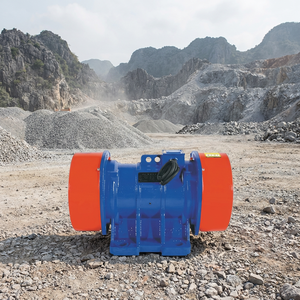
Vibrating Screen Vibrating Feeder & Hopper Vibration Motor for Ore Processing Heavy Load Capacity
Send an Inquiry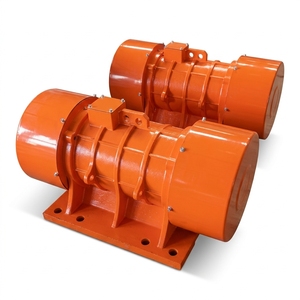
Three Phase Vibration Motor IP65 Waterproof Adjustable Exciting Force for Silo Hopper Mining
Send an Inquiry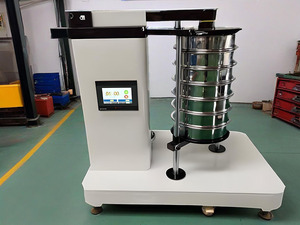
High-Accuracy Stainless Steel Laboratory Rotap Sieve Shaker Vibrating Motor Circular Screen
Send an Inquiry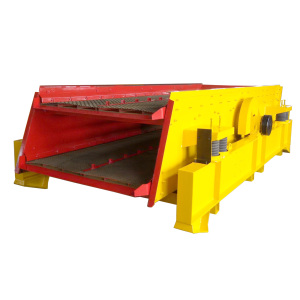
DUOLING Circular Vibrating Screen AC Motor 1-200 Tons Capacity Long Working Life Mining Bearing
Send an Inquiry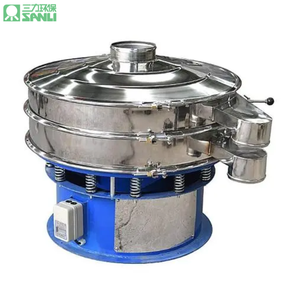
Durable Stainless Steel Rotary Vibrating Screen Motor-Easy-Clean for Processing 380V/220V
Send an Inquiry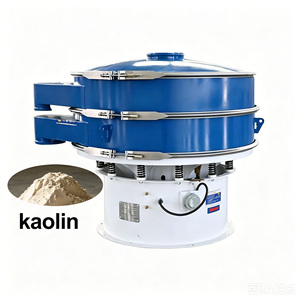
Multi-Layer Rotary Vibrating Screen Vibration Motor | 1-5 Decks Customizable | 100-500 Mesh Industrial
Send an Inquiry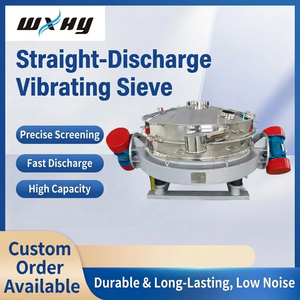
HY-1200-1s Direct Discharge Motor Vibrating Screen Heavy-Duty 380V CN Standard Motor
Send an InquiryIndustry Whitepaper: Next-Generation Engineering in Wellhead Drives & High-Frequency Vibratory Motors
In modern artificial lift artificial extraction systems—such as Progressive Cavity Pumps (PCP), Electric Submersible Pumps (ESP), and surface wellhead drive units—as well as heavy industrial processing, Wellhead Drive Motors represent the central heartbeat of operational uptime. Operating in harsh environmental conditions characterized by extreme thermal cycling, volatile hydrocarbons, corrosive media, and continuous high axial dynamic loading, selecting a qualified manufacturing supplier and global exporter is a mission-critical engineering decision.
Mechanical Dynamics & Severe-Duty Enclosures
Wellhead extraction sites and bulk material screening processing share common operational stressors: uninterrupted 24/7 duty cycles under varying load profiles. Traditional electric motors frequently fail in these environments due to insulation breakdown caused by voltage spikes (dV/dt) from Variable Frequency Drives (VFDs) or mechanical fatigue induced by uncontrolled radial vibration.
Advanced wellhead drive motors manufactured by industry leaders incorporate vacuum pressure impregnation (VPI) with specialized epoxy resins, cast-iron frame construction (NEMA 449T frame and Above NEMA sizes), and precision-balanced rotors dynamically tuned to eliminate harmonic vibration. Furthermore, adjustable eccentric weights integrated into three-phase vibration motors allow engineers to fine-tune centrifugal force outputs, ensuring seamless synchronization across multi-deck vibrating screens, hoppers, and slurry separation plants.
Unrivaled Enterprise Advantage & Global Standard Compliance
Building upon a distinguished manufacturing history established in 1901, our engineering facility in Warrior, Alabama delivers custom electric drive solutions, factory recertified units, and OEM replacement components for the world’s most demanding energy, mining, and military infrastructure.
Whether engineering specialized high-torque wellhead drives up to 20,000 HP, high-frequency Georator power converters, or explosion-proof three-phase vibration motors, our facility executes stringent quality control protocols governed by ISO 9001:2015 standards.
Technical Comparison: Standard Motors vs. Industrial Severe-Duty Wellhead Drives
Evaluating key architectural differentiators across continuous load performance, thermal resistance, and structural longevity.
| Performance Specification | Standard Commercial Motors | Industrial Severe-Duty Wellhead & Vibratory Drives |
|---|---|---|
| Insulation System | Class F (155°C limit, standard dipping) | Class H VFD Inverter-Duty (VPI treated, dV/dt resistant spike protection) |
| Bearing Configuration | Standard Deep Groove Ball Bearings | Heavy-Duty Spherical Roller / High Thrust Bearings (ISO VG 220 Synthetic Grease) |
| Ingress Protection (IP) | IP44 / IP54 (Basic dust/splash guard) | IP65 / IP66 Hermetically Sealed (Triple-lip oil seals & labyrinth slingers) |
| Frame & Structure | Rolled Steel or Light Aluminum Sheet | High-Tensile Cast Iron (FC250 / Ductile Iron) with Reinforced Ribbing |
| VFD Speed Turndown | 4:1 Constant Torque | 20:1 Constant Torque / 1000:1 Variable Torque with Encoder Feedback |
| Exciting Force Adjustment | Fixed / Non-Adjustable | Stepless Adjustable Eccentric Block Counterweights (0-100% Force Spectrum) |
Future Procurement Trends in Wellhead & Drive Motor Technology (2025–2030)
Key technological shifts shaping global B2B procurement strategies for energy producers, OEM equipment manufacturers, and mining syndicates.
1. IoT Predictive Telemetry & Digital Twins
Procurement mandates are shifting toward drive motors integrated with wireless tri-axial vibration sensors and internal stator RTDs (Resistance Temperature Detectors). Real-time telemetry prevents catastrophic downhole pump or screen bearing failures by detecting micro-fractures and thermal runaway weeks before physical breakdown.
2. Ultra-High Efficiency (IE4/IE5) Compliance
With global ESG standards and rising field electricity tariffs, energy extraction facilities are rapidly replacing legacy NEMA Energy Efficient motors with Super Premium Efficiency (IE4) and Ultra-Premium (IE5) Permanent Magnet Synchronous Motors (PMSM), reducing power consumption by up to 14%.
3. Modular Modular Seal & Quick-Exchange Flanges
To reduce field maintenance downtime, modern wellhead motors feature modular mechanical seal assemblies and standardized universal mounting flanges. Field technicians can execute seal replacements in under 45 minutes without removing the primary motor casing from the wellhead flange.
Frequently Asked Procurement & Engineering FAQs
Addressing critical buyer inquiries regarding sizing, exciting force calculation, explosion-proof ratings, and export logistics.
What primary engineering parameters must be specified when sourcing a wellhead drive motor?
When procuring a wellhead or severe-duty electric drive, engineers must specify: (1) Continuous Horsepower / Kilowatt rating, (2) Voltage & Frequency tolerance (e.g., 380V/460V/690V at 50Hz/60Hz), (3) Hazardous Location Classification (ATEX, IECEx, or UL Class I, Div 1/2), (4) Thrust Load Capability for vertical shaft configurations, and (5) VFD speed turndown ratio requirements.
How does adjustable exciting force function in three-phase vibration motors?
Three-phase vibration motors feature adjustable eccentric weights installed on both ends of the rotor shaft. By adjusting the relative angle between the inner and outer eccentric blocks, operators can smoothly adjust the centrifugal force output from 0% to 100%. This flexibility allows custom tuning for varying material densities on vibrating screens, hoppers, and aggregate separators.
Why is Class H insulation essential for VFD-driven industrial motors?
Variable Frequency Drives control motor speed using Pulse Width Modulation (PWM), which generates high-frequency voltage spikes (dV/dt) and localized thermal stress. Class H insulation systems, coupled with magnet wire featuring corona-resistant enamel coatings, ensure the motor operates reliably under ambient temperatures up to 180°C without insulation degradation.
What is the typical operational MTBF for severe-duty vibratory and wellhead motors?
Under recommended lubrication intervals (using high-temperature synthetic grease) and within specified thermal operating bands, premium severe-duty motors demonstrate a Mean Time Between Failures (MTBF) exceeding 45,000 continuous operating hours. Heavy-duty spherical roller bearings are rated for L10h bearing life exceeding 50,000 hours.
Can custom shaft extensions and mounting dimensions be engineered for legacy retrofits?
Yes. Custom electrical and mechanical engineering is a core capability. Motors can be manufactured with specialized shaft diameters, keyways, face-mount C-flanges, D-flanges, or custom foot-print dimensions to ensure drop-in replacement compatibility with legacy OEM installations without requiring field structural modification.
What international export certifications and packaging protocols are provided for global shipments?
All export machinery is compliant with ISO 9001 quality audits and can be certified to CE, UL, CSA, and ATEX standards upon request. Products are vacuum-sealed with desiccant packs, secured in heavy-duty IPPC-fumigated wooden crates, and protected with anti-corrosion barrier coatings for oceanic container transport.
Need a Custom Wellhead Drive or Vibratory Motor Specification?
Our senior application engineering team is ready to evaluate your technical parameters, structural dimensions, and electrical load profile to deliver optimized, heavy-duty drive solutions.