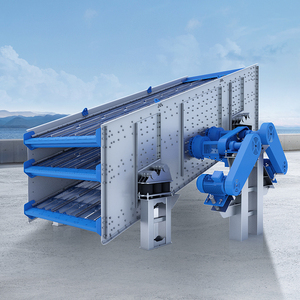
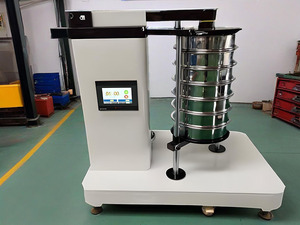
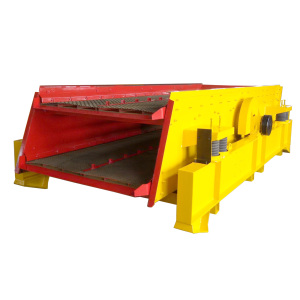
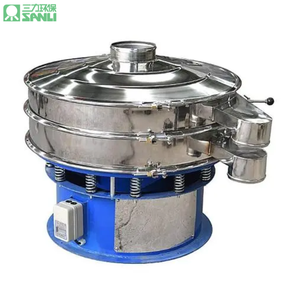
Aggregate Vibrating Screen Machine for Stone Crusher Plant 60-350t/h Ore Processing 30kW Motor High Output Finished Sand
Capacity: 60-350t/h | Motor: 30kW Heavy Duty | Application: Ore & Aggregates
Send an Inquiry
Engineered for extreme continuous duty, mining dewatering, aggregate classification, and heavy slurry circulation. Certified under ISO 9001:2015 and international IEEE/NEMA mechanical standards.
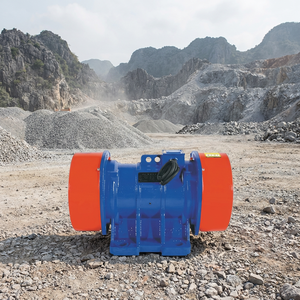

An authoritative evaluation of electromechanical performance, thermal stress mitigation, fluid dynamics integration, and bearing reliability in heavy industrial pumping and screening operations.
High-flow pumping systems operating in flood control, municipal wastewater, power generation cooling towers, and mining pit dewatering demand electric motor drives capable of absorbing extreme axial and radial thrust loading. Unlike standard NEMA general-purpose induction motors, true high-flow pump motors integrate oversized angular contact thrust bearings, dual spherical roller bearings, and precision-machined heavy-wall cast iron frames.
When pumping slurries or high-volume fluids exceeding several thousand gallons per minute (GPM), hydraulic instability, cavitation pulses, and transient back-pressures exert severe dynamic forces back through the motor shaft. Premium suppliers utilize computer-modeled finite element analysis (FEA) to verify rotor shaft stiffness, preventing shaft deflection from degrading mechanical seal integrity and preventing premature stator-rotor air gap contact.
Continuous heavy-duty operation (S1 continuous rating) under variable flow conditions requires advanced thermal management. High-flow pump motors and heavy-excitation vibratory motors utilize Class H vacuum pressure impregnated (VPI) insulation systems operating well within Class B temperature rise limits. This thermal safety margin protects copper windings against localized hotspots caused by current harmonics when driven by Variable Frequency Drives (VFDs).
To eliminate destructive bearing currents caused by Common Mode Voltage (CMV) generated by pulse-width modulated (PWM) inverters, modern high-flow pump motors are engineered with insulated non-drive-end (NDE) bearings and shaft grounding rings. This prevents electrical discharge machining (EDM) pitting inside bearing raceways, extending operational life beyond 100,000 continuous operating hours.
Comparative electromechanical specs for industrial procurement planning and plant optimization.
| Performance Specification | High Flow Centrifugal / Axial Pump Motors | Heavy-Excitation Vibratory Screen Motors | High-Precision Stainless Laboratory Motors |
|---|---|---|---|
| Primary Mechanical Duty | Continuous Hydrodynamic Thrust (S1 Duty) | Continuous High-G Acceleration (Vibratory Excitation) | Precision Micro-Frequency Separation |
| Horsepower Range | 15 HP to 20,000 HP (Medium/High Voltage) | 0.5 kW to 30 kW (Low Voltage 3-Phase) | 0.12 kW to 2.2 kW (Single/3-Phase) |
| Protection Rating | IP55, IP56, IP66, or Submersible (IP68) | IP65 Waterproof / Dust-Tight Sealed | IP66 / IP69K Easy-Clean Hygienic |
| Bearing Architecture | Angular Contact Thrust + Heavy Roller Bearings | Specialized C3/C4 Clearance Vibratory Bearings | Sealed Stainless Ball Bearings (NSK/SKF) |
| Insulation & Thermal Class | Class H VPI Insulation (Class B Rise) | Class F/H High-Vibration Epoxy Cast Winding | Class F Food-Grade/Lab Thermal Rating |
| VFD & Inverter Integration | Mandatory Inverter Duty (NEMA MG1 Part 31) | Frequency Tuned Excitation Control | Micro-Processor Step Speed Control |
| Primary Target Sectors | Water Treatment, Mining Dewatering, Power, O&G | Mining Ore, Sand/Gravel, Cement, Bulk Handling | Pharma, Food Sieving, Laboratory Particle Analysis |
Key shifts transforming global supply chains, energy efficiency compliance, and predictive maintenance protocols for enterprise equipment buyers.
Global regulatory mandates across North America, Europe, and Asia-Pacific are enforcing transition toward IE4 (Super Premium Efficiency) and IE5 (Ultra-Premium) motor standards. Procurement teams for high-flow water treatment and continuous pumping plants are prioritizing high-efficiency permanent magnet synchronous motors (PMSM) and synchronous reluctance motors (SynRM). Operating 24/7, high-flow pump motors often consume their initial capital purchase cost in electrical power within the first 6 to 9 months of continuous operation. Transitioning to IE4/IE5 ratings yields tens of thousands of dollars in lifecycle power cost reductions per motor unit.
Modern industrial buyers are moving away from reactive maintenance toward smart, sensor-integrated motor drives. Next-generation high-flow pump motors and heavy vibratory screen drives are being built with embedded multi-axis tri-axial accelerometers, RTD temperature sensors inside stator slots, and wireless IIoT mesh transmitters. These sensors continuously stream real-time vibration spectral data, bearing temperature gradients, and winding thermal signatures directly to cloud analytics platforms. Maintenance engineers can detect bearing cage degradation, imbalance, or hydraulic cavitation weeks before catastrophic mechanical breakdown occurs.
With expanding offshore mining, aggressive chemical processing, and coastal desalination infrastructure, high-flow pump motors must endure hostile chemical exposures. Future procurement specifications increasingly demand 316L stainless steel housings, nickel-plated rotors, ceramic-coated bearing seats, and specialized epoxy-phenolic marine coatings tested to withstand 5,000-hour salt spray exposure. Military-grade sealing standards (such as MIL-STD-2037 Navy sealed windings) are gaining traction in industrial heavy slurry and mining applications to protect copper windings against moisture ingress and chemical breakdown.
Backed by over a century of electromanufacturing expertise, specialized custom engineering, and rigorous ISO 9001:2015 quality control facilities.
Carrying forward the storied Louis Allis heritage since 1901, our engineering facility in Warrior, Alabama manufactures, remanufactures, and custom-engineers Above-NEMA AC and DC motors up to 20,000 HP for heavy industries worldwide.
Every motor project adheres to strict international standards including NEMA MG, IEEE, EASA-AR100, UL listings, and MIL-SPEC standard testing to guarantee reliable execution in high-consequence operational environments.
Specializing in exact fit-and-function replacement motors for obsolete legacy frames. We engineer drop-in electrical and structural duplicates that match existing mounting dimensions, shaft extensions, and terminal box locations without costly plant piping redesign.
Our factory recertified electric motors offer immediate off-the-shelf availability, fully load-tested under simulated operating conditions and backed by robust factory warranties to minimize unplanned industrial downtime.
Featuring sealed winding insulation systems certified for underwater immersion and severe chemical washdown environments. Developed for naval defense and adopted across tough industrial processing plants.
Our rapid-response field engineering team provides predictive maintenance, laser shaft alignment, dynamic balancing, failure analysis, and emergency outage support directly at your operating facility worldwide.
Use this engineering checklist when specifying equipment quotes to prevent costly misapplication and reduce Total Cost of Ownership (TCO).
Expert technical responses to common engineering, maintenance, and international export inquiries.
High-flow pump motors are specifically engineered to endure high continuous radial and axial thrust loads generated by large volumetric fluid movement. They feature specialized thrust bearings (such as angular contact ball bearings or spherical roller thrust bearings), reinforced end-bells, VPI insulation systems, and precision-balanced rotors designed for continuous S1 duty under turbulent fluid back-pressure.
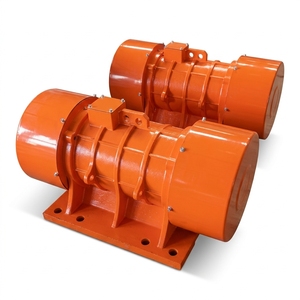
Excitation force is adjusted by altering the relative angle between the adjustable eccentric weights and the fixed eccentric weights located at both ends of the double-extended rotor shaft. By loosening the locking bolts and rotating the outer adjustable weight relative to the inner fixed weight (typically marked with percentage scale plates from 0% to 100%), operators can precisely tune the centrifugal vibration force to match material screening throughput requirements.
Mining aggregate vibrating screens operate in severe environments filled with abrasive airborne dust and water spray. Minimum protection recommended is IP65 (dust-tight and protected against water jets) or IP66 (protected against powerful water jets). In addition, windings should feature epoxy encapsulated washdown coating and mechanical seals with dual-lip oil seals to prevent dust slurry ingress into the bearing cavity.
Yes, provided the motor is specified as "Inverter Duty" compliant with NEMA MG1 Part 31 standards. Operating standard motors on VFDs without proper insulation can cause voltage spike breakdown of wire insulation and bearing fluting due to shaft currents. Inverter duty high-flow pump motors feature Class H VPI insulation, insulated non-drive end bearings, and shaft grounding brushes to ensure long-term reliability.
Factory recertified motors provide an immediate solution to long lead times common with brand-new medium and high-voltage motors. Recertified motors undergo complete disassembly, stator rewinding, mechanical machining back to OEM tolerances, dynamic rotor balancing, and 100% full-load testing under ISO 9001:2015 quality procedures. They offer identical reliability and factory warranty coverage at reduced capital expense and fast turnaround.
Our engineering team performs comprehensive dimensional and electrical reverse engineering on legacy or obsolete motor frames. We engineer custom drop-in replacement units that match your original motor's shaft centerline height, mounting hole pattern, conduit box location, and electrical performance curves. This eliminates expensive field piping modifications, structural baseplate re-engineering, and extended installation downtime.
Consult with our application engineers for custom motor design, technical datasheets, factory recertified inventory, or immediate quotation on global shipments.
Send an Inquiry