High-Performance Conveyor Drive & Vibration Motor Lineup
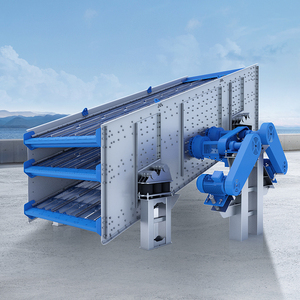
Custom engineered for heavy ore processing, aggregate vibrating screens, food sieving, and continuous industrial handling. Built to survive extreme ambient temperatures and abrasive environments.
A Heritage of Power, Precision, & Heavy-Duty Customization
Operating with a rich legacy dating back to 1901, our facility (integrating the celebrated engineering heritage of Louis Allis, a WorldWide Electric Company) stands at the pinnacle of specialty electric motor manufacturing. From our state-of-the-art ISO 9001:2015 certified production hub in Warrior, Alabama, we design, engineer, custom-fabricate, and overhaul electric drive motors up to 20,000 HP.
Whether your operational framework demands high-torque asynchronous AC motors for bulk aggregate handling, explosion-proof DC motors for underground mining hoists, or MIL-SPEC compliant drives for specialized defense installations, our engineering team ensures uncompromised mechanical reliability.
Engineering Architecture of Conveyor & Vibratory Drive Motors
Conveyor drive systems operate under continuous mechanical shock, eccentric radial torque, and harmonic vibrations that rapidly destroy conventional general-purpose motors. To achieve zero unplanned downtime in 24/7 aggregate mining, cement handling, and processing plants, custom OEM/ODM motor manufacturing requires rigorous structural mechanics and thermal management.
Finite Element Stress Modeling
Our ductile iron (FCD-450) and cast-steel end brackets undergo rigorous Finite Element Analysis (FEA) to eliminate resonance frequency overlaps. This prevents structural housing fractures caused by continuous centrifugal forces up to 50G.
Class H/H+ VPI Insulation System
Windings utilize 100% copper magnet wire treated with Vacuum Pressure Impregnation (VPI) high-temperature epoxy resins. This renders stator windings impervious to moisture ingress, dust, chemical exposure, and thermal degradation up to 180°C.
Heavy-Duty Spherical Roller Bearings
Specifically specified for eccentric motion, we integrate oversized C3/C4 clearance spherical roller bearings with high-viscosity synthetic grease. This yields an L10h fatigue life exceeding 40,000 continuous operating hours.
Technical Benchmark: Standard Motors vs. Heavy OEM/ODM Conveyor Drives
Below is a comparative breakdown illustrating why off-the-shelf electric motors fail prematurely in vibratory screening and conveyor driving applications:
| Specification Feature | Standard Commercial Motors | Our OEM/ODM Heavy Drive Motors | Operational Benefit |
|---|---|---|---|
| Bearing Construction | Standard deep-groove ball bearings | C3/C4 Brass-Cage Spherical Roller Bearings | Resists heavy radial vibration & shaft deflection |
| Insulation & Sealing | Class F varnish dipping (IP54 / IP55) | Class H VPI Epoxy resin (IP65 / IP66 / IP69K) | Prevents moisture, dust washdown & coil shorting |
| Excitation Adjustment | Fixed eccentric mass (non-adjustable) | Stepless adjustable eccentric weight blocks | Precision tuning of vibration amplitude & flow rate |
| Housing Structure | Thin-wall aluminum or standard gray iron | High-tensile FCD-450 Ductile Iron / 316 SS | Zero fatigue cracking under continuous high G-forces |
| Thermal Dissipation | Passive cooling fins | Optimized aerodynamic external rib design | Maintains temperature under 65°C continuous load |
Future Procurement Trends in Industrial Drive Motor Systems
Global bulk material handling and mining industries are experiencing a seismic shift toward smart, sustainable, and ultra-reliable powertrain technologies. Key procurement trends shaping global factory contracts include:
Transition to IE4 & IE5 Super Premium Efficiency
With industrial energy tariffs escalating globally, procurement directors are phasing out IE2/IE3 drive motors. Modern OEM contracts mandate IE4 ultra-premium and IE5 permanent magnet synchronous motor (PMSM) designs to cut operational power expenditure (OPEX) by up to 14% annually.
IIoT Condition Monitoring & Smart Sensors
Future-proof conveyor installations now require pre-drilled threaded sensor ports for IIoT tri-axial accelerometers and RTD thermal sensors. Real-time telemetry feeds cloud platforms, allowing predictive maintenance algorithms to flag bearing wear long before catastrophic line failure occurs.
Modularity & Rapid Field Maintenance
To shrink Mean Time to Repair (MTTR), procurement managers favor drive motors engineered with quick-release terminal boxes, interchangeable eccentric weights, and universal foot-mounting patterns that mirror international NEMA and IEC footprints.
Extreme Environment Hygiene & Anti-Corrosion
In food sieving and chemical processing, factories are replacing painted steel motors with crevice-free 316L stainless steel rotary units capable of enduring aggressive caustic washdown routines without flaking or chemical corrosion.
Next-Generation Technology & Development Trends
As conveyor automation speeds increase and material densities vary dynamically, motor manufacturing is evolving toward adaptive kinetic powertrain control.
1. Permanent Magnet Synchronous Vibration Motors (PMSM)
Unlike traditional induction vibration motors that experience slip under load, PMSM vibration motors maintain exact synchronous speed regardless of voltage fluctuations or surge feeding. This guarantees consistent screening frequency and precise grain sizing in silica sand, kaolin clay, and aggregate plants.
2. Direct-Drive In-Line Sieving Powertrains
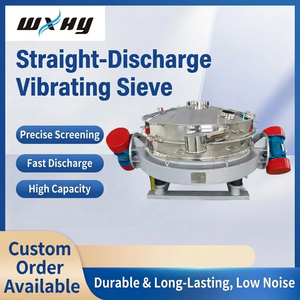
Elimination of belt drives, pulleys, and external gearboxes is a growing design trend. Direct-discharge motors (such as the HY-1200 series) pass processed material directly through the center axis, increasing flow-through velocity by up to 250% while reducing floor footprint.
3. Eco-Friendly Thermal Management & Recyclability
Next-generation factory designs incorporate non-toxic, bio-degradable synthetic greases alongside fully recyclable copper and rare-earth magnetic cores. This lowers environmental audit impact for global enterprise mining organizations.
Frequently Asked Questions for OEM/ODM Conveyor Motor Sourcing
Essential technical, operational, and commercial insights to streamline your engineering evaluation and procurement decisions.
Q1: What parameters are required to customize an OEM vibration or conveyor drive motor?
To provide precise engineering designs, we require: (1) Target exciting force (kN) or working moment (kg.cm), (2) Operating speed (RPM/Poles, e.g., 2-pole 3000/3600 RPM vs 4-pole 1500/1800 RPM), (3) Voltage & Frequency (e.g., 380V/460V/660V at 50Hz/60Hz), (4) Mounting dimensions/footprint, and (5) Ambient environment exposure (waterproof IP rating, explosion-proof ATEX/UL rating).
Q2: How do you adjust the exciting force on your three-phase vibration motors?
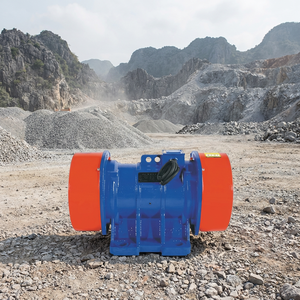
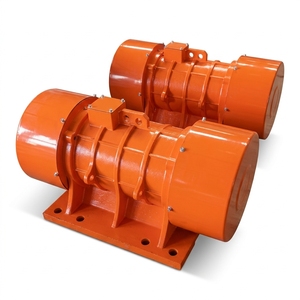
Our vibration motors feature adjustable eccentric weight blocks on both shaft ends. By loosening the outer retaining bolt and rotating the adjustable outer weight block relative to the fixed inner block, operators can seamlessly tune the centrifugal output force from 0% up to 100% capacity.
Q3: Can your factory produce motors matching specific NEMA, IEC, or legacy footprints?
Yes. As a specialty custom manufacturer with over 120 years of engineering pedigree, we routinely execute "Fit, Form, and Function" drop-in replacements. We manufacture custom shaft extensions, specialized flange adapters, and custom terminal box locations matching obsolete or legacy motors without modifying your existing machinery.
Q4: What insulation and varnish processes are used to prevent vibration breakdown?
All custom drive motors utilize Class H or Class H+ magnet wire and phase insulation. Stators undergo full Vacuum Pressure Impregnation (VPI) with 100% solid epoxy resin, followed by high-temperature oven baking. Winding heads are mechanically tied and reinforced to prevent coil movement caused by intense cyclic vibration.
Q5: What is the typical lead time for custom OEM prototyping vs mass production?
Engineered prototypes or one-off custom designs typically ship within 3 to 5 weeks depending on casting requirements. Mass OEM production runs are delivered on streamlined 4-to-6-week production cycles, supported by stocking programs for scheduled just-in-time (JIT) contract deliveries.
Q6: Are your food-grade rotary vibrating screen motors fully compliant with washdown protocols?
Yes. Our stainless steel rotary vibrating motors feature smooth, 316-grade polished surfaces without dirt-trapping pockets, oil seals rated to IP69K, and FDA-approved food-grade greases. They safely withstand daily high-pressure chemical washdowns in starch, flour, and pharmaceutical applications.
Accelerate Your Machinery Performance with Custom OEM Powertrains
Whether you need a high-output 30kW aggregate screening drive, an IP65 waterproof silo hopper vibrator, or a complete custom OEM production run built to exact engineering tolerances, our technical team is ready to consult on your project.
ISO 9001:2015 Certified Manufacturing Facility | Engineering & Global Outage Field Support | Custom Motors up to 20,000 HP