Industry Whitepaper & Technical Sourcing Guide

Custom OEM Wound Rotor Induction Motors Factories & Suppliers

High-Torque Slip Ring Motor Engineering, Global Procurement Trends & Industrial OEM Solutions

Featured OEM Vibration & Heavy-Duty Motors

Industrial Drive & Screen Motor Systems

Explore our precision-engineered heavy-load vibration motors, slip ring compatible drives, and custom processing screen machinery optimized for mining, aggregate, and raw material handling.

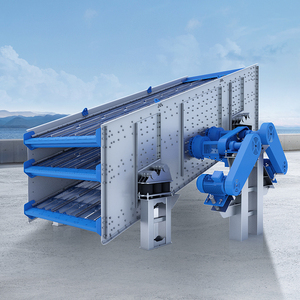
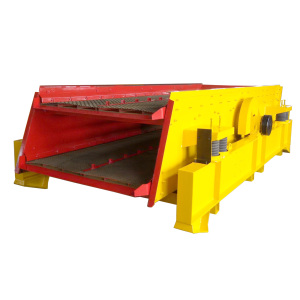
Aggregate Vibrating Screen Machine 30kW Motor

Aggregate Vibrating Screen Machine for Stone Crusher Plant 60-350t/h Ore Processing 30kW Motor High Output Finished Sand

Send an Inquiry
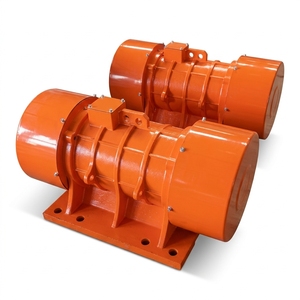
Vibrating Screen Vibrating Feeder Hopper Motor

Vibrating Screen Vibrating Feeder & Hopper Vibration Motor for Ore Processing Heavy Load Capacity Durable Engine

Send an Inquiry
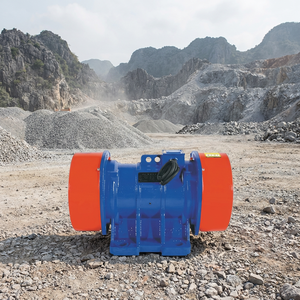
Three Phase Vibration Motor IP65 Waterproof

Three Phase Vibration Motor IP65 Waterproof Adjustable Exciting Force for Vibrating Screen Silo Hopper Mining Cement Machinery

Send an Inquiry
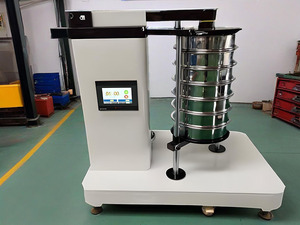
Stainless Steel Laboratory Rotap Sieve Shaker Motor

High-Accuracy Stainless Steel Laboratory Rotap Sieve Shaker Vibrating Motor Circular Vibrating Screen for Particle Size

Send an Inquiry
DUOLING Circular Vibrating Screen AC Motor

DUOLING Circular Vibrating Screen AC Motor 1-200 Tons Capacity Long Working Life for Ore Core Component Bearing Mining Screening

Send an Inquiry
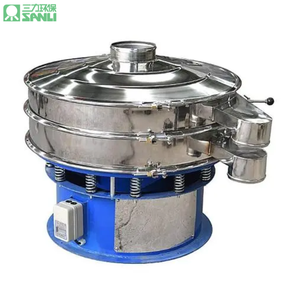
Durable Stainless Steel Rotary Vibrating Screen Motor

Durable Stainless Steel Rotary Vibrating Screen Motor-Easy-Clean for Food Processing (Dried Fruit Wheat Flour Sieving)-380V/220V

Send an Inquiry
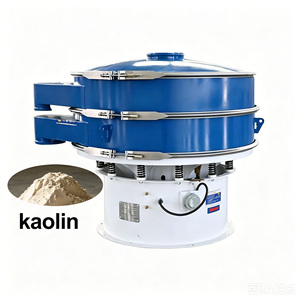
Multi-Layer Rotary Vibrating Screen Vibration Motor

Multi-Layer Rotary Vibrating Screen Vibration Motor | Kaolin Clay Processing | 1-5 Decks Customizable | 100-500 Mesh Industrial

Send an Inquiry
HY-1200-1s Direct Discharge Motor Vibrating Screen

HY-1200-1s Direct Discharge Motor Vibrating Screen 380V Industrial Grade Processing Unit

Send an Inquiry
120+
Years Industry Engineering
20,000 HP
Max AC/DC Power Rating
ISO 9001
2015 Quality Certified
MIL-SPEC
Navy Sealed Windings

1. Executive Summary & Electromechanical Fundamentals of Wound Rotor Induction Motors

In high-inertia, continuous-duty industrial applications such as ball mills, primary crushers, mining hoists, large pumps, and heavy-duty screening plants, electric motors must deliver immense starting torque while controlling locked-rotor current draw. Wound Rotor Induction Motors (WRIM), historically referred to as Slip Ring Motors, remain the premier electromechanical solution when variable starting resistance and soft acceleration under load are paramount.

Unlike standard squirrel-cage induction motors where the rotor bars are permanently short-circuited by end rings, a Wound Rotor Induction Motor features a three-phase rotor winding connected through conductive slip rings and carbon brushes to an external resistance bank or liquid rheostat. By dynamically altering the resistance inserted into the rotor circuit during startup, electrical engineers can precisely manipulate the motor's torque-speed curve, drawing maximum breakdown torque right at zero RPM without thermal overload or grid voltage drop.

Key Technical Information Gain: Rotor Resistance vs. Inrush Current

Standard squirrel-cage motors exhibit inrush currents reaching 600% to 800% of Full Load Amps (FLA) with starting torques around 150% FLA. By comparison, a custom engineered OEM Wound Rotor Induction Motor utilizing an external liquid resistance starter (LRS) limits starting current to 150%–200% FLA while delivering up to 250% full starting torque, drastically reducing mechanical stress on gearboxes and power transformers.

1.1 Structural Architecture: Stator, Slip Rings, and Brush Systems

The core reliability of a custom OEM Wound Rotor Induction Motor relies on heavy-duty structural components built to withstand intense radial vibration and thermal cycling. Key engineering components include:

VPI Vacuum Pressure Impregnation

Class H and Class H+ insulation systems treated with 100% solid epoxy resins ensure moisture barrier integrity, anti-chemical protection, and extreme mechanical strength against electromagnetic forces during heavy startups.

Precision Slip Ring Assemblies

Machined from high-conductivity bronze alloys or cupronickel alloys, equipped with spiral groove technology to equalize surface contact temperature and minimize spark formation across high-altitude and dust-heavy operations.

Constant-Force Brush Rigging

Spring-loaded electro-graphitic brush holders designed to maintain uniform contact pressure, minimizing electrical wear and brush bounce under severe heavy vibration environments found in crushers and vibrating screens.
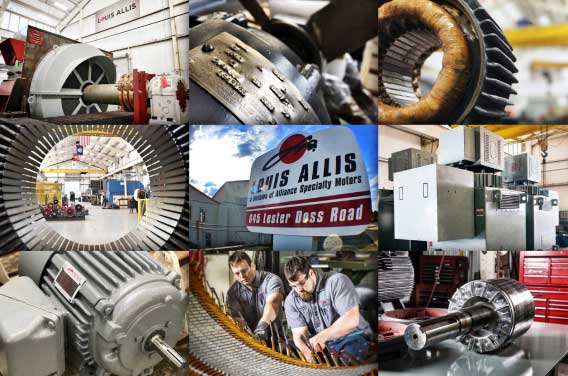
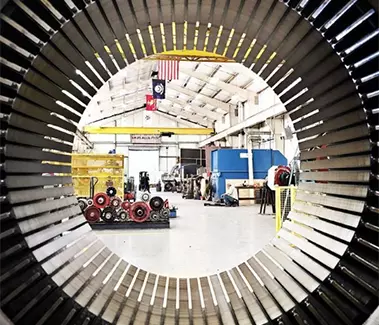
Louis Allis Specialty Motor Manufacturing Facility
Factory Excellence & History

Over 120 Years of Heritage in Custom Specialty Electric Motors

Operating from our ISO 9001:2015 certified facility, our partner engineering heritage dates back to 1901. We specialize in custom OEM engineering, complete remanufacturing, and drop-in electrical/mechanical replacement of Above NEMA AC and DC motors up to 20,000 HP.

Whether you require custom shaft modifications, special foot-print mounting adapters, MIL-STD-2037 Navy sealed windings, or EASA-AR100 precision rebuilds, our facility engineered solutions eliminate plant downtime across power generation, mining, and oil & gas sectors.

2. Technical Comparison: Wound Rotor vs. Squirrel Cage vs. VFD Drives

Selecting the optimal motor topography for large industrial machinery requires evaluating mechanical torque, electrical power quality impact, capital cost, and maintenance requirements. The comparative matrix below outlines key engineering criteria:

Engineering Metric Custom OEM Wound Rotor (WRIM) Standard Squirrel Cage (NEMA B/C) Squirrel Cage + High-Power VFD
Starting Torque Capability Up to 250% Full Load Torque 130% – 170% Full Load Torque 150% – 200% (Sensorless Vector)
Inrush Current Impact 150% – 200% FLA (Controlled) 600% – 800% FLA (High Impact) 100% – 110% FLA (Controlled)
Harmonic Distortion (THD) Near Zero (Pure Sine Wave) Near Zero High (Requires Active Front End filters)
High-Inertia Thermal Dissipation Thermal heat dissipated in external rheostat Heat absorbed inside internal rotor bars Internal heat generated during long acceleration
Capital Cost (CapEx) for >1000 HP Moderate (Proven Durability) Low initial motor cost Very High (Drive + Transformer + Filter)
Harsh Operating Environment Fit Exceptional (High Dust / IP65 enclosures) High Vulnerable VFD clean-room requirement

3. Future Procurement & Global Technological Trends (2025–2035)

As global industrial facilities strive for energy efficiency, decarbonization, and operational reliability, the procurement landscape for OEM Wound Rotor Induction Motors is evolving rapidly. Sourcing directors and plant engineering managers must adapt to four pivotal trends:

3.1 Slip Energy Recovery Systems (SERS) & Modern Hybrid Rotor Inverters

Historically, energy absorbed by rotor resistance banks during starting or speed regulation was dissipated as waste heat. Modern OEM factories are engineering Wound Rotor Induction Motors paired with Slip Energy Recovery Systems (SERS). By integrating static inverter drives into the rotor circuit, slip energy is fed back into the main AC power grid. This technology enables up to 30% speed regulation with net system efficiency exceeding 96%, creating a compelling Return on Investment (ROI) for heavy pump, fan, and kiln applications.

3.2 IoT Integration & Predictive Brush Gear Condition Monitoring

Unplanned downtime caused by brush flashover or slip ring degradation is being virtually eliminated by smart sensor deployment. Next-generation custom OEM slip ring motors feature built-in optical brush wear detectors, wireless rotor temperature telemetry, continuous vibration spectrum analysis, and online partial discharge sensors. Real-time data streams to plant SCADA systems, alerting maintenance crews long before friction or sparking disrupts production.

3.3 Drop-In Replacement Engineering for Legacy Motors

Thousands of heavy industrial sites worldwide operate aging slip ring motors manufactured 40 to 60 years ago. Today's primary sourcing strategy focuses on Exact Fit & Function OEM Reverse Engineering.

Top-tier factories do not force plant modifications. Instead, engineering teams utilize 3D laser scanning to match historical bedplate footprints, shaft center heights, terminal box locations, and voltage specs while upgrading internal insulation to modern Class H VPI standards.

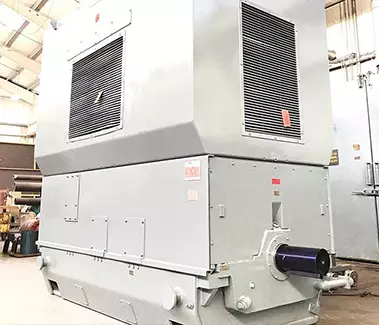
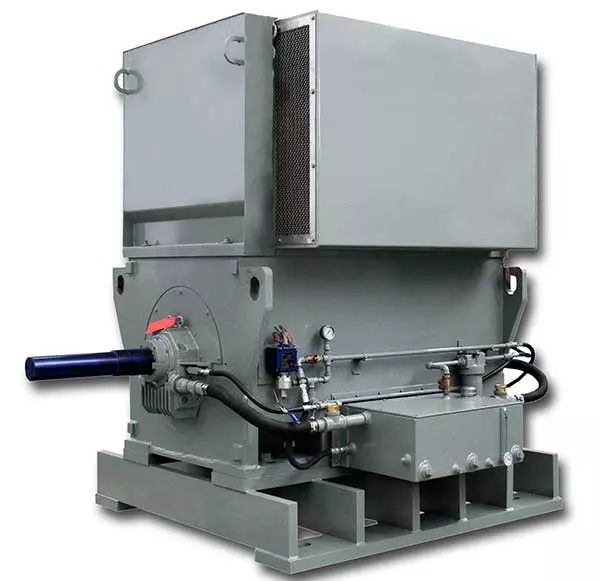
Custom Engineered Specialty Motor OEM Build

3.4 Nearshoring and Strategic Spare Motors Inventory

Supply chain bottlenecks over recent years have shifted global procurement from "Just-in-Time" to "Just-in-Case". Major mining and cement conglomerates are increasingly partnering with ISO 9001:2015 manufacturing facilities capable of holding recertified backup motors, spare rotor assemblies, and slip ring replacement modules in domestic stock to guarantee under-24-hour dispatch during unplanned outages.

4. Our Custom OEM Manufacturing & Engineering Capabilities

When selecting a custom Wound Rotor Induction Motor supplier or factory partner, technical expertise and rigorous quality testing are non-negotiable. Our engineering setup delivers custom solutions tailored precisely to high-torque and high-vibration applications:

Custom Mechanical Redesign

Complete mechanical flexibility including customized shaft dimensions, keyway specs, non-standard mounting foot patterns, heavy-duty spherical roller bearings, and IP55 to IP66 weatherproof enclosures.

Rigorous Quality Testing

Every custom motor undergoes full load surge testing, high-potential (Hi-Pot) testing, core loss evaluation, dynamic balancing to ISO 1940 G1.0 standards, and full vibration spectrum reporting prior to shipment.

Global Field Service & Repair

Complete emergency outage support, field diagnostic crews, in-situ slip ring machining, and dynamic balancing available worldwide to eliminate continuous operational losses.

Factory Recertified Electric Motors Stock
Electric Motor Replacement OEM Parts

5. Comprehensive Procurement & Technical FAQ

Key technical questions addressed by senior motor engineering directors to assist procurement managers and EPC contractors during project specification:

Q1 Why are Wound Rotor Induction Motors preferred over Variable Frequency Drives (VFDs) for heavy ball mills and crushers?

While VFDs offer excellent speed control, large high-power VFDs above 2,000 HP introduce significant harmonic distortion into the power grid and require air-conditioned clean rooms. Wound Rotor Motors utilize simple, robust liquid starters to generate maximum starting torque without electrical noise or heat buildup in electrical switchgear rooms.

Q2 What custom OEM modifications can your factory implement for legacy slip ring replacements?

We offer total mechanical and electrical drop-in matching. This includes exact shaft diameter and extension length, custom foot-hole patterns, terminal box flange matching, specialized ambient temperature designs (-40°C to +60°C), and upgraded Class H VPI insulation systems.

Q3 How often should slip ring assemblies and carbon brushes be inspected under heavy mining duty?

Under continuous 24/7 heavy-duty industrial cycles, brush gear should undergo visual and dimensional inspection every month. Brush length, spring tension (typically maintained at 2.0–2.5 psi), and slip ring surface patina should be verified quarterly to prevent micro-arcing and surface pitting.

Q4 Can custom Wound Rotor Motors be operated in explosion-proof or hazardous IP65 environments?

Yes. OEM factories engineer totally enclosed pipe-ventilated (TEPV), totally enclosed air-to-air cooled (TEAAC / IP55/IP56), or pressurization systems (Class I, Div 2 / ATEX Zone 2) with spark-proof brush enclosures specifically engineered for petrochemical and dusty mining locations.

Q5 What quality standards govern the manufacturing and rebuilding of your custom OEM motors?

Our manufacturing and remanufacturing processes comply strictly with ISO 9001:2015 certified protocols, NEMA MG-1, IEEE 841, IEEE 1415, EASA-AR100 standards, and optional MIL-STD-2037 specifications for naval-grade sealed winding insulation.

Q6 What is the typical lead time for custom engineered Above NEMA slip ring motors?

Custom ground-up OEM builds typically range from 12 to 20 weeks depending on frame size and horsepower rating. However, utilizing our extensive inventory of factory recertified frames and customizable core stock, emergency lead times can be compressed to 4 to 6 weeks.

Ready to Engineer Your Custom Motor Solution?

Speak directly with our senior electromechanical engineering team for technical CAD drawings, data sheets, drop-in replacement evaluations, or factory quote requests.

Send an Inquiry