Heavy Duty Servo & Severe-Duty Vibration Motor Solutions
Explore our OEM-grade custom servo assemblies, high-excitation vibration motors, and heavy-duty industrial drives. Built to deliver exceptional torque density, structural resilience, and long working life across mining, aggregate, chemical, and bulk material processing.
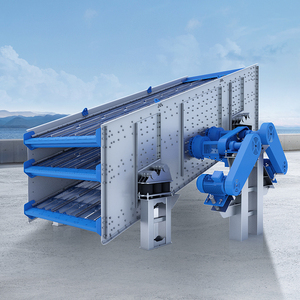
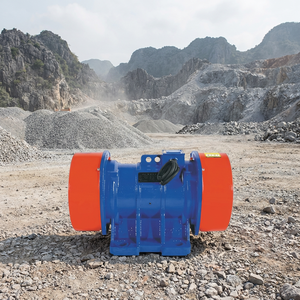
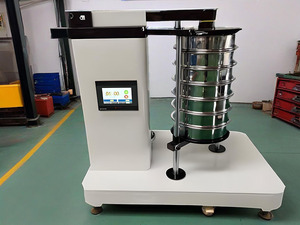
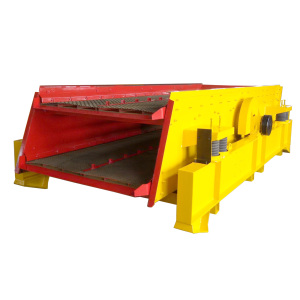
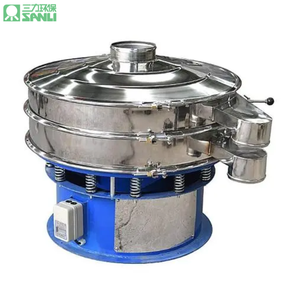

Engineering Next-Generation Heavy Duty Servo Motors for Extreme Industrial Applications
In modern high-throughput industrial operations—ranging from heavy mining vibratory screens and stone crushing aggregate plants to sub-micron powder sieving and high-load automated machinery—the demand for Custom OEM Heavy Duty Servo Motors has transitioned from standard rotary motion drivers to highly specialized, severe-duty electro-mechanical actuators.
Standard off-the-shelf servo motors frequently fail when subjected to continuous severe shock loads, high torsional vibration amplitudes, ambient heat spikes above 60°C, and ingress of abrasive particulate matter. As a premier custom OEM manufacturer rooted in over a century of electric motor design heritage, our engineering facility bridge the gap between absolute positional precision and rugged industrial survivability.
1. High-Density Permanent Magnet Synchronous (PMSM) Stator Design
Our custom OEM heavy duty servo motors utilize ultra-high-coercivity Rare-Earth Neodymium-Iron-Boron (NdFeB) and Samarium-Cobalt (SmCo) permanent magnets. Engineered with optimized slot-pole combinations, these rotors mitigate cogging torque to virtually zero while maintaining peak torque output up to 300% of nominal rating under heavy shock loading.
2. Class H & Class N Vacuum Pressure Impregnation (VPI)
Thermal degradation is the primary vector for motor insulation breakdown in high-duty cycle industrial processes. We apply military-grade Class H (180°C) and Class N (200°C) dual-layer VPI insulation systems with specialized anti-flashover varnishes, ensuring complete void-free resin fill for superior dielectric strength and rapid heat dissipation.
3. Vibration-Proof Enclosure & Heavy-Duty Bearing Arrays
Integrating heavy-duty cylindrical roller bearings paired with deep-groove angular contact ball bearings pre-loaded under dynamic springs. Shafts are precision-machined from high-tensile alloy steel (e.g., 4140/4340 or 316 Stainless) to resist high radial forces present in vibrating screens and heavy belt feeder drives.
Technical Benchmark Comparison: Standard Industrial Servo vs Custom OEM Heavy Duty Servo
Selecting the correct motor architecture is essential for minimizing Total Cost of Ownership (TCO) and avoiding un-planned line stoppages. The engineering table below highlights key functional differences between off-the-shelf servo units and our heavy-duty custom OEM solutions.
| Engineering Criterion | Standard Commercial Servo Motor | Louis Allis Custom OEM Heavy Duty Servo | Operational Impact / OEM Advantage |
|---|---|---|---|
| Peak Torque Multiplier | 150% – 200% Nominal (for < 2 seconds) | 300% – 450% Nominal (S3 duty cycle ready) | Prevents stall trips during material surges and high-inertia startup conditions. |
| Vibration Survivability | 2.5G – 4.5G Maximum Acceleration | 15G – 30G Continuous Harmonic Vibration | Essential for vibratory screeners, rock crushers, and severe impact loaders. |
| Insulation Class | Class F (155°C rise) | Class H (180°C) or Class N (200°C) VPI | Extends motor operational lifespan by 400% in elevated ambient temperatures. |
| Ingress & Corrosion Protection | IP65 Aluminum Housing | IP67 / IP68 / IP69K Cast Iron or 316 Stainless | Zero water or dust ingress under high-pressure chemical washdowns or outdoor weather. |
| Feedback System Integrity | Optical Encoders (Vulnerable to shock/glass shatter) | Heavy-Duty Heavy-Shock Resolvers / Magnetic Encoders | Eliminates optical disc failure in extreme vibration or oil-mist environments. |
| Custom Mechanical Mounting | Strict Standard NEMA / IEC Flanges Only | 100% Bespoke Shaft, Keyway, & Base Plate Geometry | Seamless direct drop-in replacement with zero retrofitting or machining required. |
Key Development Trends Driving Industrial Servo Motor Engineering
The global industrial motion control landscape is undergoing a paradigm shift. Driven by Industry 4.0 automation, decarbonization mandates, and severe-environment automation, key technological vectors are redefining heavy-duty servo motor design.
1. Smart Embedded IIoT Diagnostics
Modern heavy duty servo drives are integrated directly with tri-axial MEMS vibration sensors, thermal RTD probes, and magnetic flux monitoring arrays. Real-time predictive maintenance algorithms identify early bearing micro-spalling and phase imbalance before catastrophic failure occurs.
2. Ultra-High Energy Efficiency (IE5+)
With industrial power tariffs climbing globally, transition to Super Premium (IE4) and Ultra-Premium (IE5+) efficiency ratings is paramount. Permanent magnet synchronous servo designs eliminate rotor copper losses completely, yielding energy savings of 12% to 22% over traditional induction motors.
3. Hazardous & Explosion-Proof Certification
Mining, chemical, and flour processing equipment increasingly require explosion-proof ATEX, IECEx, and UL Class I/II Div 1 ratings. OEM heavy-duty servo motors now incorporate flame-proof joints and pressure-resistant enclosures for operating safely in combustible dust and vapor zones.
4. Direct-Drive Torque & Gearless Integration
Eliminating mechanical gearboxes through high-torque direct-drive heavy-duty servo motors eliminates back-lash, reduces friction losses, and eliminates gearbox oil leakage risks—drastically simplifying mechanical maintenance in heavy conveyors and rotary screens.
Future Procurement Trends for OEM Heavy Duty Servo Systems
Strategic procurement managers and enterprise engineering directors face evolving challenges in global supply chain risk management, total lifecycle cost control, and rapid custom prototyping. Navigating these procurement shifts requires strategic supplier alignment.
Shift from Upfront CAPEX to Total Lifecycle OPEX Evaluation
Industrial machinery buyers no longer select servo drives based purely on lowest purchase price. Evaluating motor procurement on total electrical efficiency, mean time between failures (MTBF), and spare parts standardized availability is now standard practice among Tier-1 OEMs.
Demand for Agile Custom Prototyping & Short Lead Times
Traditional electric motor manufacturers often quote 26 to 40 weeks for custom-engineered frame sizes. Leading procurement teams are partnering with agile specialized factories capable of rapid 3D CAD modeling, FEA mechanical simulation, and prototype delivery within accelerated schedules.
Nearshoring, Dual-Sourcing, & Supply Chain Resilience
Geopolitical turbulence and shipping disruptions have made dual-sourcing strategies mandatory. Procurement executives prioritize factory partners holding comprehensive in-house machining, winding, testing, and ISO quality management systems under one roof.
Over 120 Years of World-Class Electric Motor Expertise
Combining century-old American engineering tradition with state-of-the-art manufacturing technologies, our factory provides specialized custom motor manufacturing, remanufacturing, and severe-duty modification services trusted by top global industrial enterprises.
Extensive In-House Engineering & Customization
From one-off prototype specialty motors to large volume OEM production runs, our internal engineering team handles complex structural designs, custom voltage windings, mechanical mounting adaptations, and custom electrical speed-torque curves tailored exactly to your equipment specifications.
Rigorous ISO 9001:2015 & MIL-SPEC Quality Management
Every motor manufactured or rebuilt in our facility undergoes exhaustive mechanical vibration spectrum testing, full-load thermal testing, surge testing, and dielectric insulation inspection compliant with IEEE, NEMA MG1, EASA-AR100, and stringent Military standard specifications.
Severe-Duty Specialty & Emergency Outage Support
We specialize in large machinery up to 20,000 HP including specialty motors for ball mills, crushers, bow thrusters, dredge pumps, and induced draft fans. When unexpected line outages occur, our rapid-response emergency overhaul team restores operational uptime fast.
Recognized Compliance & Engineering Standards
Frequently Asked Questions (FAQ) for OEM Buyers
Comprehensive answers to common technical, mechanical, and procurement queries regarding custom heavy-duty servo motor engineering, shaft geometry, feedback protocol selection, and quality guarantees.
Require a Custom OEM Servo Motor Engineering Quote?
Connect directly with our senior application engineers to discuss custom mechanical dimensions, winding voltages, thermal ratings, or drop-in replacements for your severe-duty equipment.
Contact Us