Featured Pipeline & Industrial Vibration Motor Solutions
Engineered for continuous S1 duty, extreme fluid pressure, high vibration stability, and harsh chemical environments across mining, processing, and municipal pumping infrastructure.
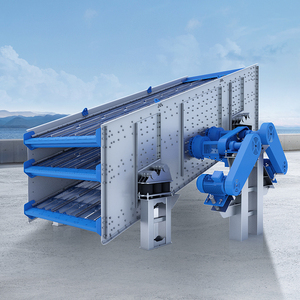
Aggregate Vibrating Screen Machine Motor (30kW Heavy Output)
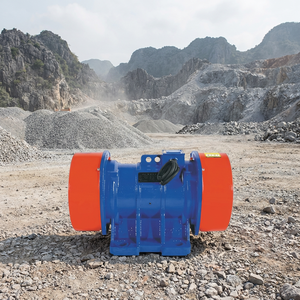
Ore Processing Heavy Load Vibration Motor & Feeder Drive
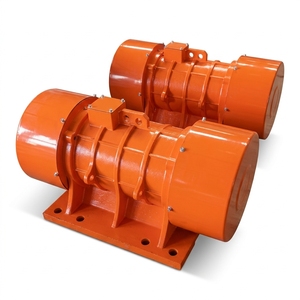
Three Phase Adjustable Exciting Force Motor (IP65 Waterproof)
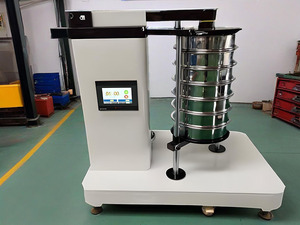
Stainless Steel High-Accuracy Precision Sanitary Shaker Motor
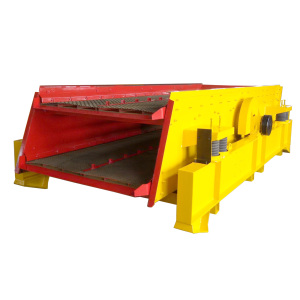
DUOLING High-Capacity AC Motor (1-200 Tons Processing)
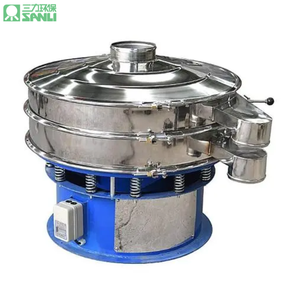
Food & Chemical Easy-Clean Rotary Stainless Steel Motor
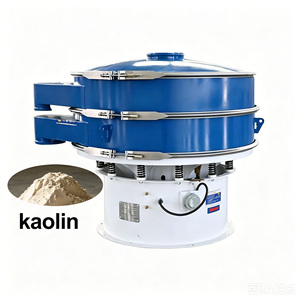
Multi-Layer Rotary Drive Motor (1-5 Decks Mesh Processing)
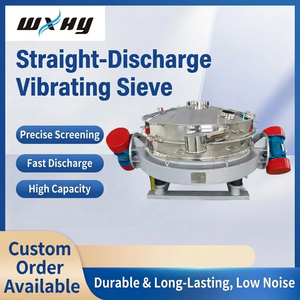
HY-1200-1s Direct Discharge High-Flow Pipeline & Screen Motor
1. Executive Summary & Global Supply Chain Landscape
In high-volume fluid transportation, oil and gas midstream infrastructure, municipal water distribution, and chemical refining, pipeline pump motors represent the critical mechanical heartbeat of global industrial fluid movement. As global industrial operations transition toward continuous processing, strict carbon neutrality mandates, and digitalized infrastructure monitoring, procurement managers and engineering executives require electric motor solutions that deliver uncompromising reliability, ultra-premium energy efficiency (IE3, IE4, and IE5 standard compliance), and low total cost of ownership (TCO).
China has established itself as the world’s preeminent manufacturing powerhouse for specialized industrial electric motors. By integrating comprehensive upstream raw material access—such as high-grade cold-rolled non-oriented electrical silicon steel, high-purity copper windings, and advanced rare-earth magnet materials—with state-of-the-art automated CNC machining facilities, China pipeline pump motor manufacturers provide unmatched supply chain resilience, competitive volume pricing, and extensive OEM/ODM engineering capabilities.
"Procuring pipeline pump motors from tier-1 Chinese manufacturers reduces capital expenditure by 30% to 45% while meeting exact IEEE 841, NEMA MG1 Premium, and IEC 60034 industrial performance benchmarks."
2. Engineering Architecture & Technical Specifications
Pipeline pump motors operate under demanding physical dynamic profiles. Unlike standard general-purpose AC motors, pipeline pump drives must accommodate continuous full-load operating cycles (S1 continuous duty), high radial and axial thrust loads transmitted from fluid impellers, and severe electrical transient spikes caused by variable frequency drive (VFD) switching frequency modulation.
Critical Structural & Electrical Components
To survive corrosive ambient environments, high relative humidity, and aggressive ambient dust, leading Chinese pump motor suppliers build motor frames utilizing heavy-gauge FC250/FC300 cast iron or 316 stainless steel. Windings are subjected to Vacuum Pressure Impregnation (VPI) with 100% solid epoxy resins, yielding Class H insulation ratings with a conservative Class B temperature rise headroom for long-term thermal durability.
| Technical Parameter | Standard Commercial Motor | Heavy-Duty Pipeline Pump Motor | Custom Explosive-Proof Pipeline Motor |
|---|---|---|---|
| Efficiency Standard | IE2 / Standard Efficiency | IE3 / IE4 Premium Efficiency | IE4 / IE5 Ultra-Premium (VFD Ready) |
| Ingress Protection | IP54 / IP55 | IP65 / IP66 Washdown | IP66 / IP67 Hermetically Sealed |
| Insulation Class | Class F (155°C) | Class H (180°C) with VPI | Class H (VPI Epoxy + Corona Inverter Guard) |
| Bearing Type | Deep Groove Ball Bearing | Re-greasable SKF/FAG Angular Contact | Insulated Hybrid Ceramic / Duplex Angular Thrust |
| Vibration Level | < 2.3 mm/s (RMS) | < 1.0 mm/s (Precision Grade A) | < 0.71 mm/s (Ultra Precision Grade B) |
| Hazardous Rating | Non-rated | Optional Class I Div 2 | ATEX / IECEx Zone 1 & 2 (Ex d IIC T4 Gb) |
VFD Inverter Spikes Protection
Integrated spike-resistant magnet wire and phase insulation shields guard against high dV/dt voltage transients generated by modern IGBT variable frequency drives.
Enhanced Bearing Load Capability
Heavy angular contact bearings and non-sparking metallic fans support continuous high hydraulic thrust forces without thermal breakdown or mechanical deflection.
Precision Dynamic Balancing
Rotors are dynamically balanced to ISO 1940-1 Grade G1.0 standards, minimizing harmonic vibrations, pump cavitation damage, and acoustic emissions.
3. Fluid Dynamics Integration & Application Scenarios
Pipeline pump motors serve across an extensive range of industrial hydraulic installations. Matching the correct motor torque curve, enclosure rating, and mounting configuration (vertical P-base vs. horizontal foot-mounted) to the specific pump type is essential to prevent operational downtime.
Primary Industry Applications
1. Crude Oil & Refined Petroleum Pipelines: Heavy-duty explosion-proof motors (ATEX/IECEx certified) configured with flameproof enclosures (Ex d IIB/IIC T4) designed to continuous main-line booster pumps.
2. Municipal & Agricultural Water Supply: High-thrust vertical hollow-shaft and solid-shaft pump motors powering deep-well submersible pumps, high-pressure booster stations, and municipal wastewater processing plants.
3. Chemical Processing & Corrosive Fluids: Stainless steel or chemical-duty cast iron motors outfitted with Fluorocarbon (Viton) lip seals, IP66 washdown protection, and epoxy internal paint systems resistant to acid and alkali vapors.
4. Mining Slurry & Tailings Transport: High-torque vibration-resistant AC motors paired with slurry pumps and vibrating screen feeders, capable of starting under heavy mineral slurry head pressures.
4. Manufacturing Excellence, Heritage & Quality Governance
Backed by over a century of heritage engineering expertise (incorporating legacy design methodologies perfected since 1901), our manufacturing facilities in China seamlessly combine time-tested electromagnetic designs with cutting-edge robotic production technologies.
Every pipeline pump motor engineered in our factory undergoes rigorous quality control inspection protocols governed by ISO 9001:2015 standards. Our testing capabilities include full-load temperature rise testing, surge comparison testing, partial discharge analysis, acoustic noise testing, and 100% hydrostatic testing for liquid-cooled housing units.
We offer comprehensive compliance certifications including CE, UL, CSA, ATEX, IECEx, and IEEE 841, assuring seamless project commissioning and regulatory compliance in North America, Europe, the Middle East, and Southeast Asia.
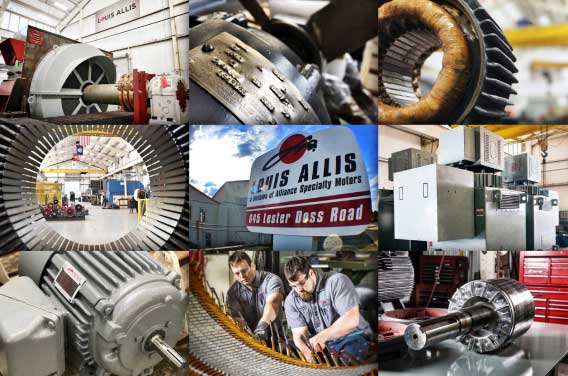
Heritage
5. Future Procurement Trends: Smart Motors & Carbon Neutrality (2025–2030)
The global pipeline pump motor market is undergoing a major technological transformation. B2B procurement leaders must align their purchasing strategies with emerging technological paradigms to avoid premature equipment obsolescence:
1. Integration of Smart IoT Condition Monitoring: Modern pipeline motors are increasingly pre-equipped with embedded tri-axial vibration sensors, temperature detectors (PT100 RTDs), and wireless Bluetooth/LoRaWAN telemetry nodes. This enables real-time cloud analytics and AI-driven predictive maintenance, preventing unexpected bearing breakdown or winding burnouts.
2. Transition to IE5 Ultra-Premium & Permanent Magnet Synchronous Motors (PMSM): While asynchronous induction motors remain industry mainstays, IE5 permanent magnet synchronous pump motors deliver up to 30% reduction in electrical losses under partial load conditions, dramatically shortening investment payback periods.
3. Modular & Compact Lightweight Designs: Utilization of high-density electromagnetic steel laminations and advanced internal air-to-water heat exchangers (TEWAC) allows up to 20% reduction in motor footprint while maintaining extreme power density.
6. Frequently Asked Questions (Procurement & Technical FAQ)