CE Certified Heavy-Duty Motors & Vibrating Machinery
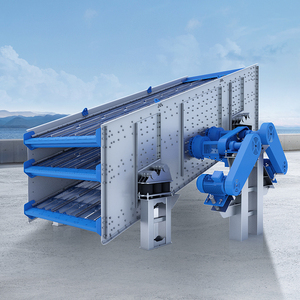
Aggregate Vibrating Screen Machine for Stone Crusher Plant 60-350t/h Ore Processing 30kW Motor High Output Finished Sand
Get Catalog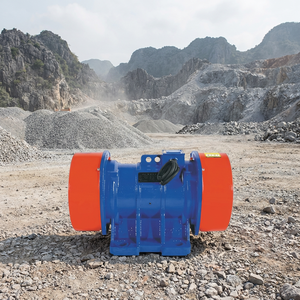
Vibrating Screen Vibrating Feeder & Hopper Vibration Motor for Ore Processing Heavy Load Capacity Durable Engine
Get Catalog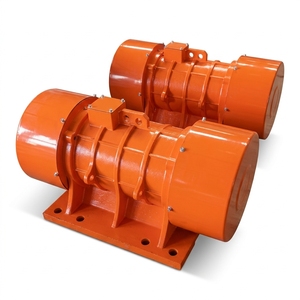
Three Phase Vibration Motor IP65 Waterproof Adjustable Exciting Force for Vibrating Screen Silo Hopper Mining Cement Machinery
Get Catalog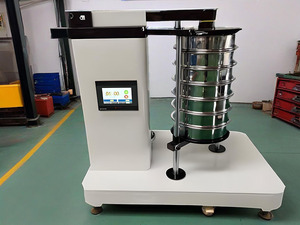
High-Accuracy Stainless Steel Laboratory Rotap Sieve Shaker Vibrating Motor Circular Vibrating Screen for Particle Size
Get Catalog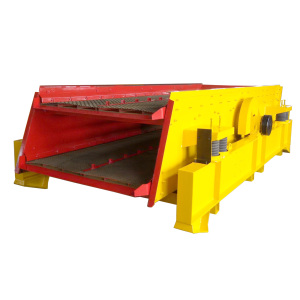
DUOLING Circular Vibrating Screen AC Motor 1-200 Tons Capacity Long Working Life for Ore Core Component Bearing Mining Screening
Get Catalog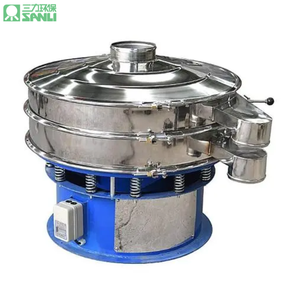
Durable Stainless Steel Rotary Vibrating Screen Motor-Easy-Clean for Food Processing (Dried Fruit Wheat Flour Sieving)-380V/220V
Get Catalog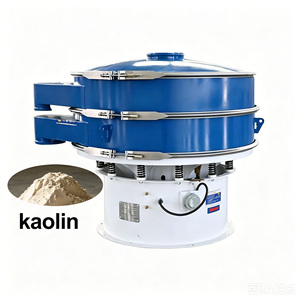
Multi-Layer Rotary Vibrating Screen Vibration Motor | Kaolin Clay Processing | 1-5 Decks Customizable | 100-500 Mesh Industrial
Get Catalog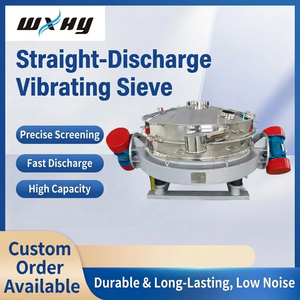
HY-1200-1s Direct Discharge Motor Vibrating Screen 380V CN Heavy Duty Slurry & Particle Handling Unit
Get Catalog1. Technical Architecture & Engineering Excellence of CE Certified Slurry Pump Motors
Operating in severe industrial fluid-handling environments—such as mineral processing tailings, dredging, coal preparation, and chemical slurry transportation—requires electric motors that far transcend standard induction designs. A true CE Certified Slurry Pump Motor represents a fusion of heavy electromechanical engineering, thermal margin optimization, and dynamic sealing barrier technology.
Slurry pumping operations expose drive systems to continuous high radial thrust, severe axial forces, abrasive airborne particulates, and high humidity. Standard industrial motors fail prematurely under these stress vectors due to bearing raceway pitting, winding insulation breakdown, and shaft deflection. Our engineering framework integrates century-old manufacturing traditions with modern finite element analysis (FEA) to engineer motor drive solutions capable of continuous S1 duty cycles under extreme specific gravity (SG up to 1.8+) fluid loads.
Core Electromechanical Engineering Specifications:
- Vacuum Pressure Impregnation (VPI) Insulation: Utilizing Class H and Class H+ solventless epoxy resins engineered to withstand transient voltage spikes (VFD-induced dv/dt) up to 1600V peak, fully compliant with NEMA MG1 Part 31 standards.
- Heavy-Duty Bearing Assemblies: Fitted with oversized SKF/NSK spherical roller and angular contact thrust bearings, calculated for an L10h bearing fatigue life exceeding 100,000 continuous operating hours.
- Shaft Voltage & Shaft Current Mitigation: Integrated insulated Non-Drive End (NDE) bearing housings and conductive micro-fiber grounding rings to completely eliminate electrical discharge machining (EDM) fluting.
- CE Safety & Compliance Directives: Manufactured in strict accordance with European Harmonized Standards, specifically the Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility Directive (EMC 2014/30/EU), backed by full third-party laboratory test documentation.
Enterprise Manufacturing Advantages & E-E-A-T Efficacy
120+ Years Engineering Pedigree
Built upon a century of manufacturing authority (Louis Allis heritage), producing specialty AC/DC industrial electric motors up to 20,000 HP for defense, mining, and heavy energy sectors.
ISO 9001:2015 & MIL-SPEC Quality
Every motor undergoes full-load testing, vibration spectrum analysis, partial discharge testing, and hydrostatic pressure testing in our ISO 9001:2015 certified Alabama facility.
Custom Fit-&-Function Engineering
Direct drop-in replacements for obsolete or hard-to-source slurry pump drive motors. Custom shaft extensions, foot print dimensions, flange geometries, and terminal box locations.
Smart VFD & IIoT Readiness
Pre-installed PT100 RTDs in stator windings and bearing housings, tri-axial vibration sensor bosses, and inverter-duty magnet wire for real-time operational diagnostics.
2. Technical Specifications Matrix: Standard vs. Heavy-Duty Slurry Motors
Selecting the correct motor geometry requires analyzing radial forces, thermal dissipation, ingress protection, and duty cycle resilience. The comparative visualization below illustrates why standard industrial motors cannot withstand aggressive slurry pump environments.
| Engineering Parameter | Standard Industrial AC Motor | CE Heavy-Duty Slurry Motor | Submersible Slurry Pump Motor |
|---|---|---|---|
| Ingress Protection Rating | IP55 (Standard Dust/Splash) | IP66 / IP67 Heavy Waterjet | IP68 Submersible (30m+ depth) |
| Insulation & Thermal Class | Class F (155°C) with Class B rise | Class H (180°C) VPI Impregnated | Class H+ Triple VPI Dip |
| Bearing Design (Drive End) | Single Row Deep Groove Ball | Oversized Roller + Thrust Bearing | Duplex Angular Contact Roller |
| Target L10h Bearing Life | 20,000 – 40,000 Hours | > 100,000 Operating Hours | > 80,000 Operating Hours |
| Shaft Sealing Architecture | Single V-Ring Rubber Seal | Dual Lip Viton Seals + Labyrinth | Mechanical Silicon Carbide Seals |
| CE & Safety Directives | Basic LVD Compliance | LVD 2014/35/EU, EMC, ATEX Zone 2/22 | CE Certified + Ex-proof IECEx |
3. Global Procurement Trends & Technological Horizons (2025–2030)
As global mining, sand/aggregate processing, and industrial wastewater treatment sectors push for decarbonization and elevated operational uptime, the market demand for premium slurry handling equipment is undergoing a major technological transformation. Procurement directors and EPC consultants are transitioning from low-initial-cost acquisition models toward Total Cost of Ownership (TCO) evaluation frameworks.
Key Market Drivers & Engineering Trends:
- Transition to IE4 & Super Premium Efficiency: With electricity accounting for over 85% of an industrial motor's lifecycle cost, European and North American procurement standards now mandate IE4 efficiency levels for continuous-duty slurry drive units, drastically cutting indirect scope 2 emissions.
- Condition Monitoring & Embedded IIoT Diagnostics: Industrial procurement specifications increasingly require factory-fitted condition monitoring packages. Modern CE certified slurry motors feature embedded vibration acceleration sensors, thermal resistance detectors (RTDs), and insulation leakage detectors linked directly to plant SCADA systems via Modbus/PROFINET protocols.
- Advanced Anti-Corrosive Coating Matrices: Mine tailings containing acidic leach solutions or saline slurry demand specialized surface treatments. Modern manufacturers apply multi-coat polyurethane and high-solid epoxy coatings exceeding 300 microns thickness, passing 1,500-hour ASTM B117 salt spray endurance testing.
- VFD Spike-Shielding Wire Innovations: As variable frequency drives become standard for adjusting slurry velocity to prevent pipeline settling, pulse-width modulation (PWM) harmonic spikes pose severe stress to motor windings. Advanced inverter-duty magnet wire utilizing organic-inorganic hybrid nano-composite coatings is becoming a mandatory procurement requirement.
4. Procurement & Technical Frequently Asked Questions (FAQ)
Addressing core technical questions from plant engineers, maintenance directors, and B2B procurement managers regarding CE certified slurry pump motors.
Request Custom Engineering Specifications & Technical Catalogs
Partner with an authoritative electric motor manufacturer backed by over 120 years of proven manufacturing heritage. Speak with our application engineering team today to review CAD drawings, thermal curves, and competitive pricing.
Get Catalog