Industrial Crusher & Screening Motor Technology Overview
Jaw crushers and industrial vibrating screens represent the most mechanically demanding applications in aggregate processing, hard-rock mining, and mineral recycling. Equipment operating in these severe-duty environments is subjected to continuous shock loads, massive transient peak torque spikes, heavy radial forces, and omnipresent abrasive dust. Selecting an engineered powertrain—specifically a CE Certified Jaw Crusher Motor or a high-excitation vibration motor—is the primary determinant of plant uptime, operational safety, and overall cost per ton processed.
As a premier direct manufacturer and global exporter, our engineering facilities integrate over a century of motor design heritage—combining Above NEMA structural robustness with precision European CE compliance (EN 60034-1) and ISO 9001:2015 quality assurance. Whether driving primary jaw crushers processing 60 to 350 tons per hour or powering multi-deck vibrating screens for particle classification down to 500 mesh, our motor architecture guarantees high starting torque, thermal margins exceeding NEMA Class H standards, and IP65/IP66 ingress protection.
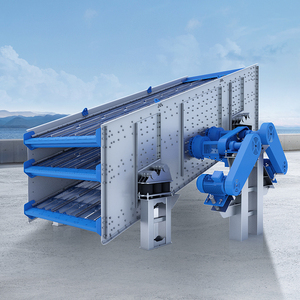
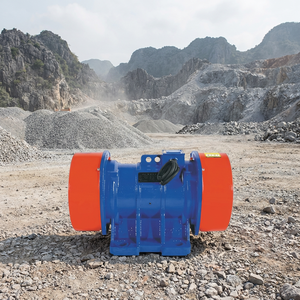
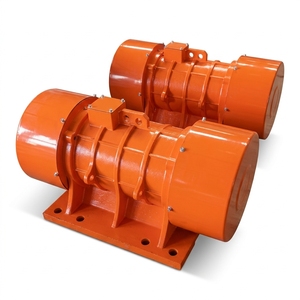
Featured Crusher Duty & Vibration Screen Motors
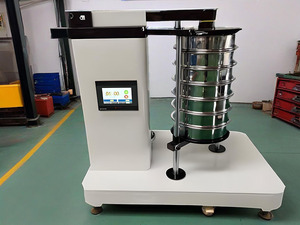
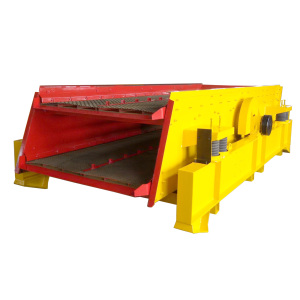
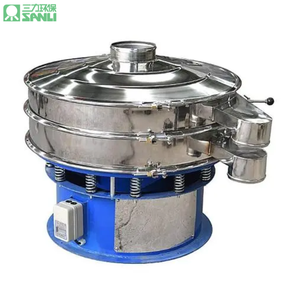
Explore our CE-certified range of heavy-duty AC induction motors, direct discharge exciters, and multi-layer rotary vibration engines optimized for mining, aggregate, and laboratory sieving.

Jaw Crusher Motor Design Principles & Shock-Load Resistance
Primary jaw crushers operate via dynamic compressive force, breaking large boulders and basalt slabs between a fixed and a moving jaw plate driven by an eccentric shaft. This mechanical action creates an exceptionally harsh electrical load profile: severe cyclic torque fluctuations occurring 200 to 300 times per minute, coupled with intense structural vibration transmitted back through the V-belt drive into the motor bearings and frame.
High Starting Torque (NEMA C/D)
Jaw crushers often must start under stalled or partially loaded pit conditions. Our motors provide 250% to 300% breakdown and locked-rotor torque, ensuring reliable startup without tripping circuit breakers or overheating rotor bars.
Vacuum Pressure Impregnation (VPI)
Stator windings undergo 100% solid solventless epoxy VPI resin processing under 100 PSI vacuum. This eliminates air voids, prevents wire-to-wire chafing from vibration, and provides Class H thermal tolerance (180°C).
Heavy-Duty Bearing Assemblies
Equipped with NU/NJ series cylindrical roller bearings or spherical roller bearings held in cast-iron endbells with steel-reinforced bearing seats to absorb overhung loads from heavy flywheels.
Engineering Specification Matrix: Crusher Duty vs. Standard Motors
| Technical Parameter | Standard Industrial Motor | CE Certified Jaw Crusher Motor | Vibrating Screen Vibration Motor |
|---|---|---|---|
| Frame Construction | Rolled Steel / Standard Aluminum | High-Tensile FC250 Cast Iron | Ductile Iron / Cast Steel Mono-Block |
| Starting Torque (LRT) | 150% - 180% Rated Torque | 250% - 320% Rated Torque | Instantaneous Direct-Excitation |
| Insulation & Temp Rise | Class F (155°C) / Class B Rise | Class H (180°C) VPI Resin Sealed | Class H VPI / Heavy Copper Wire |
| Ingress Protection | IP54 / IP55 Standard | IP65 Dust-Tight & Water Jet Proof | IP66 Fully Sealed Enclosure |
| Vibration Balance | ISO 1940 Grade G2.5 | ISO 1940 Grade G1.0 Precision | Controlled Eccentric Force Exciters |
| Duty Cycle Rating | S1 Continuous Duty | S1 Continuous Heavy Crusher Duty | S1 Continuous High-Frequency Vibration |
Future Procurement Trends for Jaw Crusher Powertrains
Global quarrying, mineral processing, and construction waste recycling sectors are undergoing rapid technological transformation. Plant managers and EPC contractors no longer evaluate motor procurement solely on initial purchase price; total cost of ownership (TCO), energy efficiency standards, and dynamic predictive maintenance capabilities now dictate global sourcing contracts.
1. Transition to IE4 & IE5 Ultra-Efficiency
With energy costs representing up to 90% of an electric motor's total lifecycle cost, global mining hubs across Europe, North America, and Australia are mandating IE4 (Super-Premium Efficiency) and IE5 (Ultra-Premium Efficiency) motors to drastically reduce continuous kWh power consumption in high-tonnage crushing plants.
2. IIoT Smart Vibration & Thermal Monitoring
Modern CE-certified crusher motors are increasingly pre-fitted with integrated tri-axial vibration sensors and PT100 RTD thermal probes. Wireless IIoT telemetry streams real-time health data to plant SCADA systems, enabling predictive maintenance before catastrophic bearing breakdown occurs.
3. Modular Customization & Drop-in Footprints
Global aggregate producers demand rapid OEM replacement capability. Leading exporters offer custom shaft extensions, dual-drilled foot mountings (Above NEMA and IEC standards), and convertible terminal box locations to ensure 100% drop-in compatibility during emergency factory outages.
Why Partner With Our OEM Motor Manufacturing Facility
With over a century of specialty electric motor design and manufacturing expertise, our state-of-the-art facilities produce heavy-duty AC and DC motors up to 20,000 HP. Operating under strict ISO 9001:2015 certified quality management systems, our products comply with MIL-SPEC, NEMA MG1, IEEE, EASA AR100, UL, and European CE standards.
Frequently Asked Questions by Mining Engineers & Buyers
Need Custom Crusher Motor Engineering or Factory Quotations?
Our senior electrical application engineers are available to review your crushing plant duty cycle, mechanical mounting requirements, or custom vibration motor specs. Contact our factory team today for direct B2B exporter pricing and worldwide delivery schedules.
Contact Us